
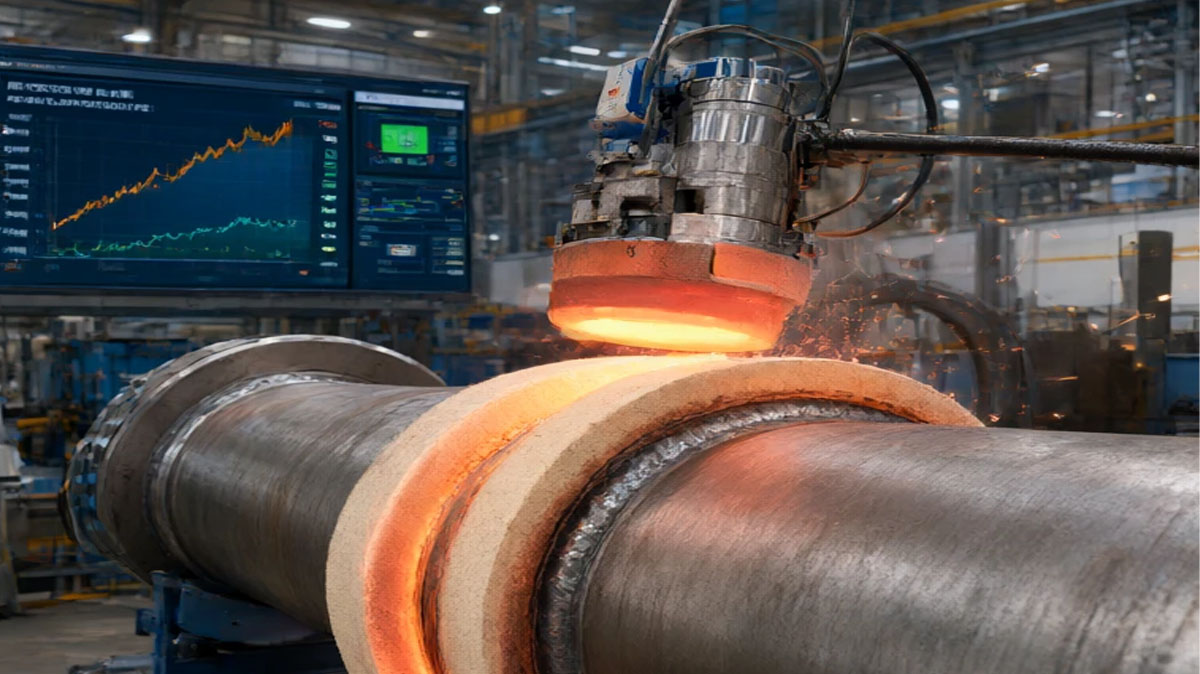
PWHT (Post‑Weld Heat Treatment) is a controlled heating and cooling process applied to welded metal to reduce residual stresses, temper hard microstructures, and improve toughness, typically required by codes such as ASME Section VIII and B31.3.
What PWHT is
Post‑Weld Heat Treatment is a thermal cycle performed after welding. It involves:
- Heating the weld and surrounding heat‑affected zone (HAZ) to a specified temperature.
- Holding (soaking) at that temperature for a defined time.
- Controlled cooling back to ambient temperature.
This process relieves stresses created during welding and tempers brittle microstructures.
Why PWHT Is Needed
PWHT addresses several welding‑related issues:
- Residual stress reduction: Welding causes contraction stresses that can approach yield strength; PWHT reduces these by 70–85%.
- Tempering hard HAZ microstructures: Rapid cooling can form martensite with hardness 350–450 HB; PWHT softens and stabilizes the structure.
- Improved toughness and ductility: Tempering improves impact resistance.
- Hydrogen removal: Helps prevent delayed cracking.
- Dimensional stability: Reduces distortion in critical components.
When PWHT Is Required
Industry codes specify mandatory PWHT based on material, thickness, and service conditions:
- ASME Section VIII (Pressure Vessels)
- ASME B31.3 (Process Piping)
- NACE MR0175/ISO 15156 (Sour Service)
- AWS D1.1 (Structural Steel) — rarely required.
Examples: - Carbon steel (P‑1): Required above ~19 mm thickness.
- Cr‑Mo alloys (P‑4, P‑5A, P‑5B): Required at higher temperatures (704–732°C).
- Sour service: Mandatory to meet hardness limits (22 HRC).
Typical PWHT Parameters
| Material Group | Typical PWHT Temp | Hold Time | Notes |
|---|---|---|---|
| Carbon steel (P‑1) | ~593°C | 1 hr per 25 mm | Required above 19 mm |
| Cr‑Mo (P‑4/P‑5A) | ~704°C | 1 hr per 25 mm | Hardness reduction |
| P91 (P‑5B) | ~732°C | ≥2 hr per 25 mm | All thicknesses |
| Austenitic SS | Not required | — | PWHT may cause sensitization |
| Duplex SS | Not required | — | PWHT degrades properties |
PWHT Methods
- Furnace PWHT: Uniform heating for shop‑fabricated spools.
- Local PWHT: Field welds using resistance pads or ceramic heaters.
- Induction PWHT: Fast, controlled heating using induction coils.
PWHT is an essential post‑welding process that improves weld reliability by reducing residual stresses, tempering hard microstructures, and ensuring compliance with engineering codes for safe service.


